

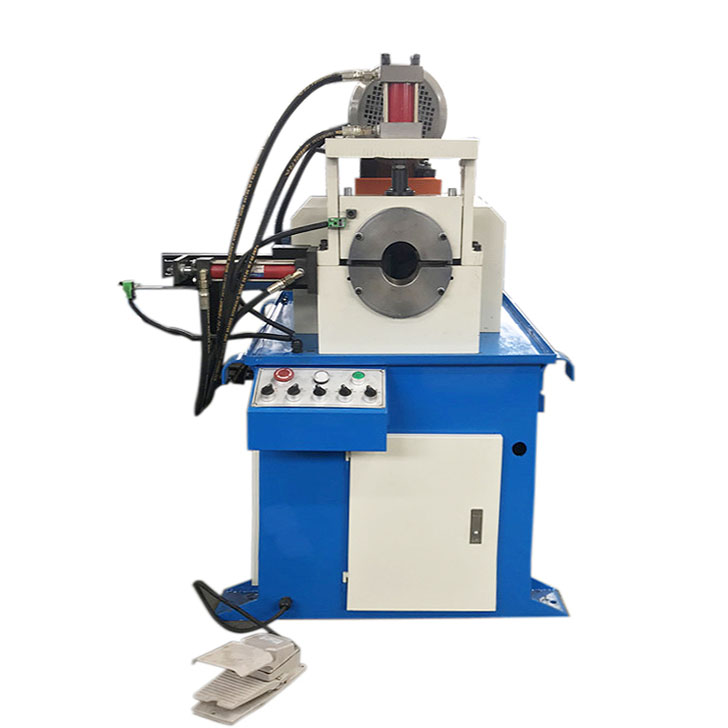
Sharp bolt edges often cause assembly problems, thread damage, and early cracking. I have seen many factories ignore this detail and lose product quality.
Bolt head chamfering improves assembly, protects threads, removes burrs, reduces stress concentration, and increases fastening stability. It is one of the most important finishing processes in bolt manufacturing.
Factories that still use outdated processing methods often struggle with low efficiency and unstable quality. I will explain how different chamfering methods work and which solution fits different bolt manufacturers.
Why Must Bolts Have Head Chamfering?
Many factories think chamfering is only cosmetic work. I once believed the same until I saw how sharp edges caused assembly failures.
Bolt chamfering creates a smooth transition on bolt edges. It improves assembly performance, reduces burrs, protects threads, and extends bolt service life under heavy loads.
Better Assembly and Faster Installation
When a bolt keeps a sharp 90-degree edge, it becomes difficult to guide into threaded holes or nuts. Workers often spend more time aligning bolts during installation. In automated production lines, sharp bolt ends can easily jam feeding systems.
After chamfering, the angled edge acts like a guide surface. The bolt enters the hole more smoothly. I have seen factories reduce assembly time immediately after improving chamfer consistency.
For industries like automotive parts, furniture hardware, and pipeline systems, smoother assembly directly improves production efficiency.
Burr Removal and Cleaner Products
Cold heading, cutting, and thread rolling often leave small burrs on bolt ends. These burrs create several hidden risks:
| Problem | Impact |
|---|---|
| Sharp metal edges | Worker injuries |
| Loose metal chips | Damage to hydraulic systems |
| Uneven surfaces | Poor product appearance |
| Burr accumulation | Thread installation issues |
Chamfering removes these sharp edges completely. The final product looks cleaner and more professional. Many overseas buyers care deeply about visual consistency because it reflects manufacturing quality.
Stress Reduction and Longer Service Life
Sharp corners easily create stress concentration under vibration or high load conditions. Over time, bolts may crack near the edge area.
Chamfering distributes stress more evenly across the bolt surface. This becomes very important for:
- Heavy machinery
- Pressure vessels
- Construction fasteners
- Aerospace parts
- Automotive suspension systems
I once visited a customer producing high-strength fasteners for engineering equipment. They experienced repeated bolt fractures during vibration tests. After improving chamfer quality, the failure rate dropped significantly.
Protecting Threads During Installation
Without chamfering, sharp bolt edges can damage threads during installation. This causes thread deformation, cross-threading, and poor locking force.
A smooth chamfer helps threads engage naturally. The installation process becomes easier and more stable.
Stronger Locking Performance
Chamfered surfaces improve contact between bolts, washers, and nuts. The force distribution becomes more even.
This is especially useful in applications where vibration resistance matters.
Why Some Factories Still Ignore Chamfering
Some small workshops still treat chamfering as an optional step because they focus only on lowering production cost.
However, buyers from Europe, North America, and the Middle East now expect much higher quality standards. A rough bolt surface immediately affects customer trust.
From my experience, proper chamfering often decides whether a customer places repeat orders.
What Chamfering Methods Do Bolt Factories Use Today?
Different factories use completely different chamfering equipment. Some still rely on manual grinding, while others use fully automated systems.
Modern bolt factories mainly use four chamfering methods: manual grinding, traditional lathes, dedicated chamfering machines, and fully automated production systems.

Method 1: Manual Grinding with Sand Wheels
This is the oldest and cheapest chamfering method.
Workers hold bolts by hand and grind the edge against a sanding wheel or handheld grinder.
Advantages
| Advantage | Details |
|---|---|
| Low investment | Equipment cost is very cheap |
| Simple operation | No advanced training needed |
| Flexible usage | Suitable for repair work |
Disadvantages
| Problem | Result |
|---|---|
| Heavy labor dependence | High labor cost |
| Poor consistency | Uneven chamfer size |
| Low efficiency | Very slow production |
| Safety risk | Worker injury possibility |
| Poor appearance | Inconsistent product finish |
I rarely recommend this method today except for very small workshops or temporary repair work.
Method 2: Traditional Lathe Processing
Many small and medium bolt factories still use ordinary lathes or instrument lathes.
The operator manually clamps each bolt, performs turning and chamfering, then unloads the workpiece.
Typical Processing Flow
- Manual loading
- Bolt positioning
- Clamping
- Turning
- Chamfering
- Unloading
Production Problems
The biggest problem is efficiency.
For short bolts, traditional manual lathe processing usually requires 25 to 35 seconds per piece.
Workers repeat the same movement all day. Fatigue quickly affects processing accuracy.
| Comparison Item | Traditional Lathe |
|---|---|
| Average cycle time | 25–35 seconds |
| Labor requirement | High |
| Skill requirement | Moderate |
| Consistency | Medium |
| Automation level | Very low |
Although lathe precision is acceptable, more factories are replacing these machines with dedicated chamfering equipment.
Method 3: Dedicated Pneumatic or Hydraulic Chamfering Machines
This is currently the most practical upgrade solution for medium and small bolt factories.
Machines like the CJ-80 pneumatic or hydraulic single-head chamfering machine are designed specifically for short bolts, shafts, and threaded workpieces.
Why Dedicated Chamfering Machines Became Popular
I have worked with many bolt manufacturers that struggled with unstable production before switching to dedicated chamfering systems.
The biggest improvement usually comes from fixture design.
CJ machines use a self-developed blind-hole fixture system. This design supports many bolt sizes without constant fixture replacement.
Main Advantages
| Feature | Benefit |
|---|---|
| Blind-hole fixture system | Compatible with many thread sizes |
| Flexible positioning | Protects workpiece surfaces |
| Fast processing speed | About 5 seconds per bolt |
| Stable chamfer quality | Better product appearance |
| Easy operation | No programming required |
| Compact size | Saves factory space |
| Low maintenance | Lower long-term cost |
Higher Efficiency Than Traditional Lathes
Compared with ordinary lathes, dedicated chamfering machines can improve production capacity by five to seven times.
This difference becomes extremely important when factories process thousands of bolts every day.
Better Surface Protection
Many factories worry about damaging threads during chamfering.
Dedicated machines use flexible limiting systems that avoid scratching threads or surfaces. This greatly improves finished product quality.
Suitable Applications
These machines work especially well for:
- Short bolts
- Stub bolts
- Shaft parts
- Pipe fittings
- Medium-batch fastener production
Method 4: Fully Automated Double-Head Chamfering Systems
Large fastener manufacturers often use fully automated chamfering lines.
These systems automatically feed bar material and process both ends at the same time.
Main Advantages
| Advantage | Result |
|---|---|
| Full automation | Very low labor cost |
| Huge production capacity | Hundreds of thousands daily |
| Stable processing | Consistent quality |
| Double-end processing | Faster cycle times |
Main Disadvantages
| Problem | Result |
|---|---|
| High machine cost | Large investment |
| Large footprint | More factory space needed |
| Limited flexibility | Poor for small-batch jobs |
| Difficult setup | Longer adjustment time |
These systems are ideal for standardized mass production but not suitable for many non-standard fastener factories.
How Should Bolt Factories Choose the Right Chamfering Process?
Many factory owners ask me the same question. Which chamfering method gives the best balance between cost, speed, and flexibility?
The best chamfering solution depends on production volume, product variety, labor cost, and required processing precision.
Small Workshops Should Eliminate Manual Grinding
Small workshops often continue using sanding wheels because the initial investment is low.
However, labor cost keeps increasing every year. Product consistency also becomes harder to control.
Even a simple dedicated chamfering machine can immediately improve:
- Worker safety
- Product appearance
- Production efficiency
- Customer acceptance rate
Medium-Sized Bolt Factories Need Flexible Solutions
For most medium-sized factories, pneumatic or hydraulic single-head chamfering machines provide the best cost-performance balance.
Why These Machines Fit Modern Fastener Factories
| Requirement | Dedicated Chamfering Machine |
|---|---|
| Multi-specification production | Excellent |
| Low training difficulty | Excellent |
| Return on investment | Fast |
| Production stability | High |
| Maintenance difficulty | Low |
Many buyers from Canada, Europe, and Mexico now prefer suppliers that can maintain stable appearance and fast delivery.
A stable chamfering process directly supports both goals.
Large Factories Should Keep Automated Lines
Factories producing standard bolts in huge quantities still benefit from fully automated chamfering systems.
These production lines work best when:
- Product specifications rarely change
- Daily production volume is very high
- Labor cost is expensive
- Long-term automation planning exists
Precision Bolts Require CNC Chamfering
Some industries require extremely high precision.
Examples include:
- Aerospace fasteners
- Medical equipment screws
- High-pressure sealing systems
- Precision automotive components
In these cases, CNC chamfering machines provide tighter dimensional control and better repeatability.
Key Factors Before Buying Chamfering Equipment
Before choosing equipment, factories should evaluate:
| Evaluation Factor | Why It Matters |
|---|---|
| Bolt size range | Fixture compatibility |
| Daily production target | Required efficiency |
| Product variation | Machine flexibility |
| Labor availability | Automation demand |
| Budget | Investment planning |
| Quality requirement | Precision level |
I always suggest focusing on long-term production stability instead of only looking at machine price.
A cheap machine with unstable performance often creates larger hidden costs later.
Conclusion
Bolt head chamfering directly affects assembly quality, thread protection, product lifespan, and factory competitiveness in modern fastener manufacturing.


